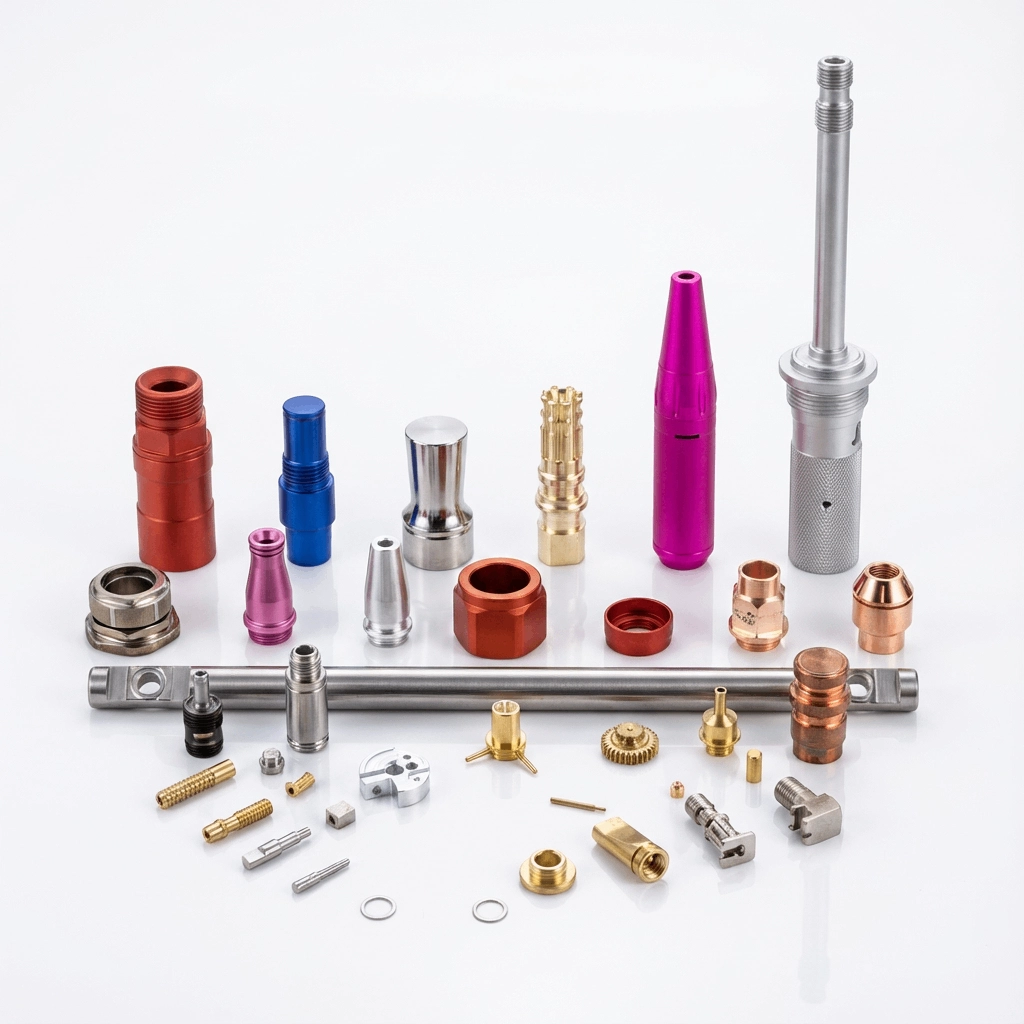
The Practical Guide to CNC Machining Materials for Precision Parts
Selecting the right CNC machining materials is the first and most critical decision in any precision manufacturing project. Over the past decade, running a job shop that serves medical device makers, semiconductor equipment builders, and automotive Tier 1 suppliers, I’ve seen how a seemingly small material choice can make or break a part’s performance, cycle time, and bottom line. This guide cuts through the marketing noise and gives you real-world data on common alloys, plastics, and when to pick one over the other.
We’ll talk about machinability, surface finish achievable (down to 0.005mm if needed), thermal stability, chemical resistance, and of course, cost. No theory without practice. And because you’re busy, I’ve added a decision logic section you can use directly in your next design review.
Key Factors in CNC Machining Materials Selection
Before we compare specific materials, let’s establish the criteria that actually matter on the shop floor.
Machinability – How easily the material cuts, chip formation, tool wear. A material with poor machinability can double your cycle time and eat up endmills.
Dimensional stability – After machining, does the part move? Stress-relieved alloys and certain plastics hold tolerances like ±0.005mm; others warp when you look at them.
Hardness & strength – Harder isn’t always better. Very hard materials (above 40 HRC) demand specialized toolpaths and rigid setups, increasing cost.
Corrosion resistance – Critical for medical implants, semiconductor wet benches, and automotive sensors exposed to road salts.
Cost per part – Material price per kilogram plus machining time. Sometimes a cheap material that’s hard to cut ends up more expensive than a premium free-machining alloy.
Application domain – Medical requires biocompatibility (ISO 13485). Semiconductor needs ultra-clean, non-outgassing materials. Automotive values fatigue strength and impact resistance.
Here’s a quick reference table I keep on my shop wall.
Medical device housings, semiconductor fixtures, automotive brackets, consumer electronics enclosures
2
Stainless Steel
303, 304, 316L, 17-4 PH
160-350
4 (303 is okay; 316L is tough)
Surgical tools, fluid handling components, sensor housings for automation
3
Brass
C36000 (free-cutting)
80-100
9 (superb)
Pneumatic fittings, valve cores, electrical connectors, decorative auto parts
2.5
Titanium
Grade 5 (Ti-6Al-4V)
330-360
2 (difficult)
Medical implants (knee/hip), high-end automotive engine components, chemical processing
5
Engineering Plastics
PEEK, Delrin (POM), Nylon 6/6, PTFE
Varies (Shore D)
6 (Delrin is easy; PEEK is moderate)
Semiconductor wafer carriers, insulating parts for consumer electronics, wear pads in automation
3.5 (PEEK is 5)
Low-Carbon Steel
12L14, 1018, 4140 pre-hard
120-300
7 (12L14 is excellent)
General machine parts, automotive shafts, brackets (non-corrosive environments)
1.5
H2: Aluminum vs. Steel – The Everyday Showdown
This is the most common question I get from procurement and design engineers: “Why would I pay more for aluminum when steel is stronger?”
The answer isn’t about strength alone. Let’s break it down.
Aluminum (6061-T6) – Our go-to for 60% of orders. It’s fast to cut, produces excellent surface finishes, and doesn’t punish tooling. We regularly hold ±0.01mm on aluminum parts for semiconductor wafer handling fixtures. The low density means lighter moving parts – critical for high-speed automation arms. Corrosion resistance is decent without coating. But it’s soft, so threaded holes strip easily, and it’s not suitable for high-wear applications like gear trains.
Steel (stainless or low-carbon) – When you need stiffness, wear resistance, or fatigue life, steel wins. A stainless steel 316L sensor housing for a medical sterilizer will outlast aluminum by decades. However, machining steel is slower. Our spindle load doubles, feeds drop by 40%, and we use carbide tools with specialized coatings (AlTiN). Also, internal stresses in rolled steel plates can cause warpage after you remove material – we always specify stress-relieved blanks for tight-tolerance steel parts.
Decision shortcut: Choose aluminum if weight, speed of manufacturing, or moderate corrosion resistance matter. Choose steel if the part sees high cyclic loads, abrasive environments, or needs to survive impacts.
For a real example: we produce a 200mm diameter vacuum chamber lid for semiconductor deposition equipment. Made from 6061-T6 aluminum because it’s non-magnetic, machines to a mirror finish, and conducts heat evenly. On the other hand, the guide rails inside an automated assembly line are 4140 pre-hard steel – because they slide against bearings 20 hours a day.
🔗 To see how we handle both materials in production, visit our CNC machining services page for case studies.
H2: Plastic vs. Metal CNC Machining – When to Ditch the Metal
Many engineers default to metal because “it’s stronger.” But plastics – especially high-performance ones – often solve problems metals can’t.
Plastic advantages:
Electrically insulating (PEEK, Delrin, PTFE) – essential for semiconductor handling tools that could short out sensitive chips.
Chemically inert (PTFE, PEEK) – stands up to aggressive cleaning solvents in medical and semiconductor fabs.
Lightweight – consumer electronics benefit from polycarbonate or ABS enclosures.
Self-lubricating (Delrin, Nylon) – perfect for bushings and sliding parts without oil.
Metal advantages:
Higher temperature resistance (stainless survives autoclave sterilization; most plastics don’t).
Structural rigidity – a metal bracket won’t creep under constant load.
EMI shielding – necessary for communication equipment housings.
Real shop insight: We once machined a batch of 500 fluid connectors for a medical dialysis machine. The customer specified 316L stainless – expensive and slow to cut. We suggested PEEK as an alternative. PEEK is biocompatible, steam-sterilizable, and machines beautifully (though it costs as much as some steels). The customer switched, saving 35% per part after factoring in faster cycle times and zero post-machining passivation.
Decision logic for plastic vs. metal:
Does the part need to conduct electricity or shield EMI? → Metal.
Will it be submerged in harsh chemicals or need to be non-stick? → PTFE or PEEK.
Does it require high stiffness under load at elevated temperatures (>150°C)? → Metal (or maybe PEEK, but verify).
Is weight critical and forces are low? → Plastic.
H2: Deep Dive – Stainless Steel, Brass, and Titanium
Let’s look at three specialized materials that show up regularly in our work for medical, automotive, and automation.
H3: Stainless Steel CNC Machining Advantages
We use three grades most often: 303 (free-machining, good for complex parts), 304 (general purpose, tougher on tools), and 316L (medical and marine grade, excellent corrosion resistance).
Advantages:
High strength and toughness even at cryogenic temperatures (relevant for semiconductor cooling loops).
Easy to clean and passivate – medical surgical guides demand this.
Readily weldable if you need assemblies.
Challenges:
Work-hardening. If your tool rubs instead of cuts, the surface hardens and destroys the next insert.
Poor thermal conductivity – heat builds up at the cutting edge, so we use high-pressure coolant (70 bar) and climb milling.
Cost reality: A 316L part might take 3x longer to machine than the same geometry in 6061 aluminum. But for a medical implant that stays in the body for 20 years, nobody cares about the extra $50 per part.
H3: CNC Machining Brass Material – The Underrated Hero
Brass (especially C36000) machines like butter. It produces beautiful, chip-free surfaces and doesn’t need coolant most of the time. We use it for:
Pneumatic fittings in automation systems (leak-tight threads).
Electrical contacts and terminals in consumer electronics (good conductivity).
Decorative trim for automotive interiors (golden finish without plating).
One caveat: brass is relatively soft and can gall if you overtighten threads. For dynamic applications with vibration, we recommend inserting a steel helicoil.
H3: CNC Machining Titanium Properties – High Reward, High Effort
Titanium Grade 5 (Ti-6Al-4V) is the darling of medical implant makers. It’s biocompatible, extremely strong for its weight, and resists corrosion better than almost anything.
What makes it hard to machine:
Low thermal conductivity – 95% of the heat stays in the tool. Without proper coolant delivery, your endmill glows red and fails in minutes.
High chemical reactivity – titanium welds itself to the tool edge at high temperatures.
Use sharp, polished carbide tools with variable flute geometry.
Keep radial engagement low (5-10% of tool diameter).
Flood coolant with extreme pressure additives.
Accept slower feed rates – typical cycle times are 4-5x aluminum.
Applications we machine regularly:
Bone plates and screws (medical) – we achieve surface finishes of Ra 0.4 µm.
Connecting rods for high-performance automotive engines.
Components for chemical sensors (automation equipment).
🔗 Need a custom run in titanium or any other material? Our custom CNC machining team can review your drawing and suggest the optimal alloy.
H2: Material Hardness and Machining – What Tolerances Can You Actually Hold?
A common myth: “Harder materials always give better precision.” Not true. In fact, very soft materials (like pure copper) are harder to hold tight tolerances because they deform under clamping pressure.
From our CMM records:
Material Hardness Range
Typical Achievable Tolerance (CNC milling)
Main Limiting Factor
< 100 HB (e.g., pure aluminum, brass)
±0.025 mm
Workpiece deflection during cut
100-250 HB (6061-T6, 303 SS, mild steel)
±0.010 mm
Machine thermal stability
250-400 HB (17-4 PH, Ti-6Al-4V, hardened steel)
±0.005 mm (possible)
Tool wear and vibration
> 400 HB (tool steels, Inconel – not typical)
±0.010 mm or worse
Tool failure risk
We regularly hold ±0.005 mm on critical features like bearing bores in 17-4 PH stainless (condition H900). That’s 5 microns – about 1/10th the thickness of a human hair. But achieving that requires a rigid setup, fresh tools, temperature-controlled coolant, and a machine that’s been warmed up for 30 minutes. The same part in soft 6061 would be harder to hold that tolerance because the material would push away from the cutter.
Takeaway: If your design needs ultra-high precision, don’t automatically pick a soft material because “it’s easier.” Sometimes a harder, more stable alloy actually makes the tolerance easier to hold.
H2: CNC Machining Material Cost Comparison – The Real Picture
Material price per kilogram is deceptive. The true cost is material price + machining time + tooling wear + secondary operations.
Let’s compare a simple block (50x50x50 mm) with a pocket and four tapped holes, quantity 100 pieces.
Material
Material cost per part (USD)
Machining time (minutes)
Tool wear cost
Total part cost (est.)
6061 Aluminum
$1.80
4.5
$0.10
$8.40
12L14 Steel
$1.20
5.0
$0.30
$8.00
316L Stainless
$4.50
12.0
$1.20
$22.20
C360 Brass
$3.00
3.5
$0.05
$9.55
Grade 5 Titanium
$18.00
18.0
$4.00
$58.00
PEEK
$22.00
6.0
$0.80
$34.80
The table above is based on our actual quoting data from Q3 2025. Notice that 12L14 steel is cheaper per part than 6061 aluminum in this case – because steel’s lower material cost offsets slightly longer cycle time. But if you need corrosion resistance, 316L jumps to $22, which might still be acceptable for a medical device that sells for $500.
Pro tip: For low-volume prototypes (1-10 pieces), material cost is almost irrelevant – focus on machinability to get parts faster. For high-volume (1000+), spend time optimizing material choice because even 10 seconds saved per part adds up.
H2: Decision Logic – How to Pick the Right CNC Machining Material in 5 Steps
I teach this to our junior engineers. Use it as a checklist.
Step 1 – Define the primary function. Is the part structural? Electrical? Thermal? Fluid-handling? Aesthetic? Write it down.
Step 2 – Identify environmental threats.
Moisture / salt? → Stainless, brass, or coated aluminum.
High temperature (>150°C)? → Metal or PEEK (up to 250°C).
Chemicals (acids, solvents)? → 316L, PTFE, or PEEK.
Sterilization (autoclave, gamma)? → Titanium, 316L, or PEEK.
Step 3 – Consider production volume.
1-50 pcs: Choose the most machinable material that meets requirements (e.g., 6061 aluminum or 303 stainless).
50-500 pcs: Start optimizing cycle time – maybe switch from 316L to 303 if corrosion resistance allows.
500+ pcs: Run a formal cost comparison including tool life. Consider free-machining grades like 12L14 or C360 brass.
Step 4 – Check geometric complexity.
Thin walls (<1 mm) or deep cavities? Avoid gummy materials (pure copper, low-carbon steel with no sulfur). Use aluminum or brass.
Threads smaller than M2? Use brass or 303 stainless – they won’t break taps.
Tight tolerances (≤ ±0.01 mm) on large surfaces? Use pre-stress-relieved alloy steel or 7075 aluminum.
Step 5 – Add secondary operations.
Need anodizing? Only aluminum.
Need passivation? Stainless steel.
Need electroless nickel plating? Almost any metal, but avoid brass if you need high adhesion.
Need bonding or ultrasonic welding? Plastics like ABS or polycarbonate.
Apply these five steps to your next part, and you’ll avoid the classic mistake of over-specifying (paying for titanium when 6061 works) or under-specifying (using plain steel in a medical implant).
H2: Industry-Specific Material Preferences
From our actual order history (no aerospace, per our policy).
Fatigue strength, cost-effective, good machinability for high volume
Automation equipment
6061 aluminum, Delrin (POM), 303 stainless, brass
Low friction, dimensional stability, easy to modify
Note: For semiconductor, we never use materials that outgas sulfur or chlorine – that disqualifies many standard plastics and some low-grade steels. We only machine certified clean materials with full traceability.
H2: People Also Ask (PAA) – Quick Answers
Q1: What is the easiest metal to CNC machine? Free-cutting brass (C360) and 6061 aluminum are the easiest. They produce short chips, don’t work-harden, and allow aggressive feed rates up to 0.25 mm/tooth.
Q2: Can you CNC machine PEEK like metal? Similar strategies, but PEEK requires sharp tools and proper chip evacuation. Use coolant to prevent melting. PEEK’s low thermal expansion helps hold tight tolerances, sometimes better than aluminum.
Q3: Which CNC machining material is cheapest? Low-carbon steel (like 12L14) has the lowest material cost per kilogram. But if you add post-machining plating or heat treatment, aluminum can become cheaper overall.
Q4: Why is titanium so expensive to machine? Low thermal conductivity (heat stays in the tool), high chemical reactivity (welding to cutter), and high strength require slow speeds, rigid setups, and frequent tool changes. Cycle times are typically 4-5x aluminum.
Q5: Is stainless steel harder to machine than regular steel? Yes, most stainless grades (especially 304 and 316) work-harden and have lower thermal conductivity. Free-machining 303 is closer to mild steel, but still slower than 12L14.
Q6: What material gives the best surface finish in CNC machining? Brass and aluminum (with polished tools) can achieve Ra 0.2-0.4 µm. For plastics, Delrin machines to a glass-like finish. Steel requires secondary grinding or polishing for mirror surfaces.
Q7: How do I choose between 6061 and 7075 aluminum? 7075 is stronger (570 MPa ultimate tensile vs 310 MPa for 6061) and harder, but less corrosion resistant and more expensive. Use 7075 for highly stressed automotive or aerospace parts (though we don’t do aerospace). Use 6061 for everything else.
Q8: Can you machine brass without coolant? Yes, for light cuts. Brass chips carry heat away. But for production runs or deep holes, use mist or flood coolant to prevent chips from packing.
Ready to start
Your next project?
Contact our technical experts today for a customized solution and a tailored quotation.
Our expert team will contact you within 24 hours
to provide a free technical evaluation and solution design, helping you upgrade your production process.
ADDRESS
NO.22,You Yi Road ,Wulian Community, LongCheng Street ,Long gang District ,Shen Zhen